Reactors
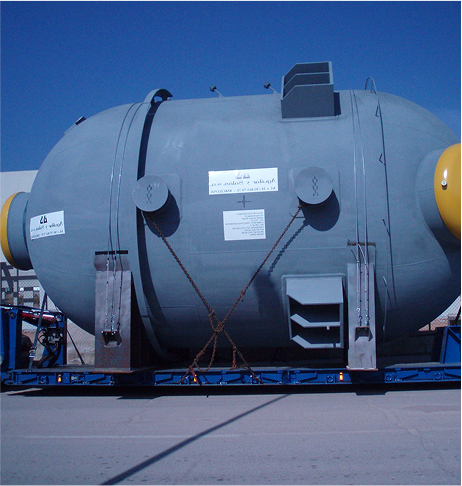
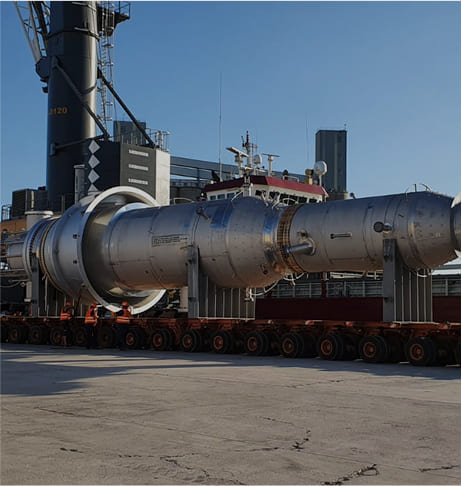
We manufacture reactors with high precision, ensuring durability and compliance with strict industry standards. As a trusted industrial reactor manufacturer, InoxTorres designs and builds custom reactors in stainless steel, high-nickel alloys, duplex, superduplex, cladding, and titanium — engineered for the pressure, temperature, and corrosion-resistance demands of the chemical, petrochemical, pharmaceutical, and fine chemical industries.
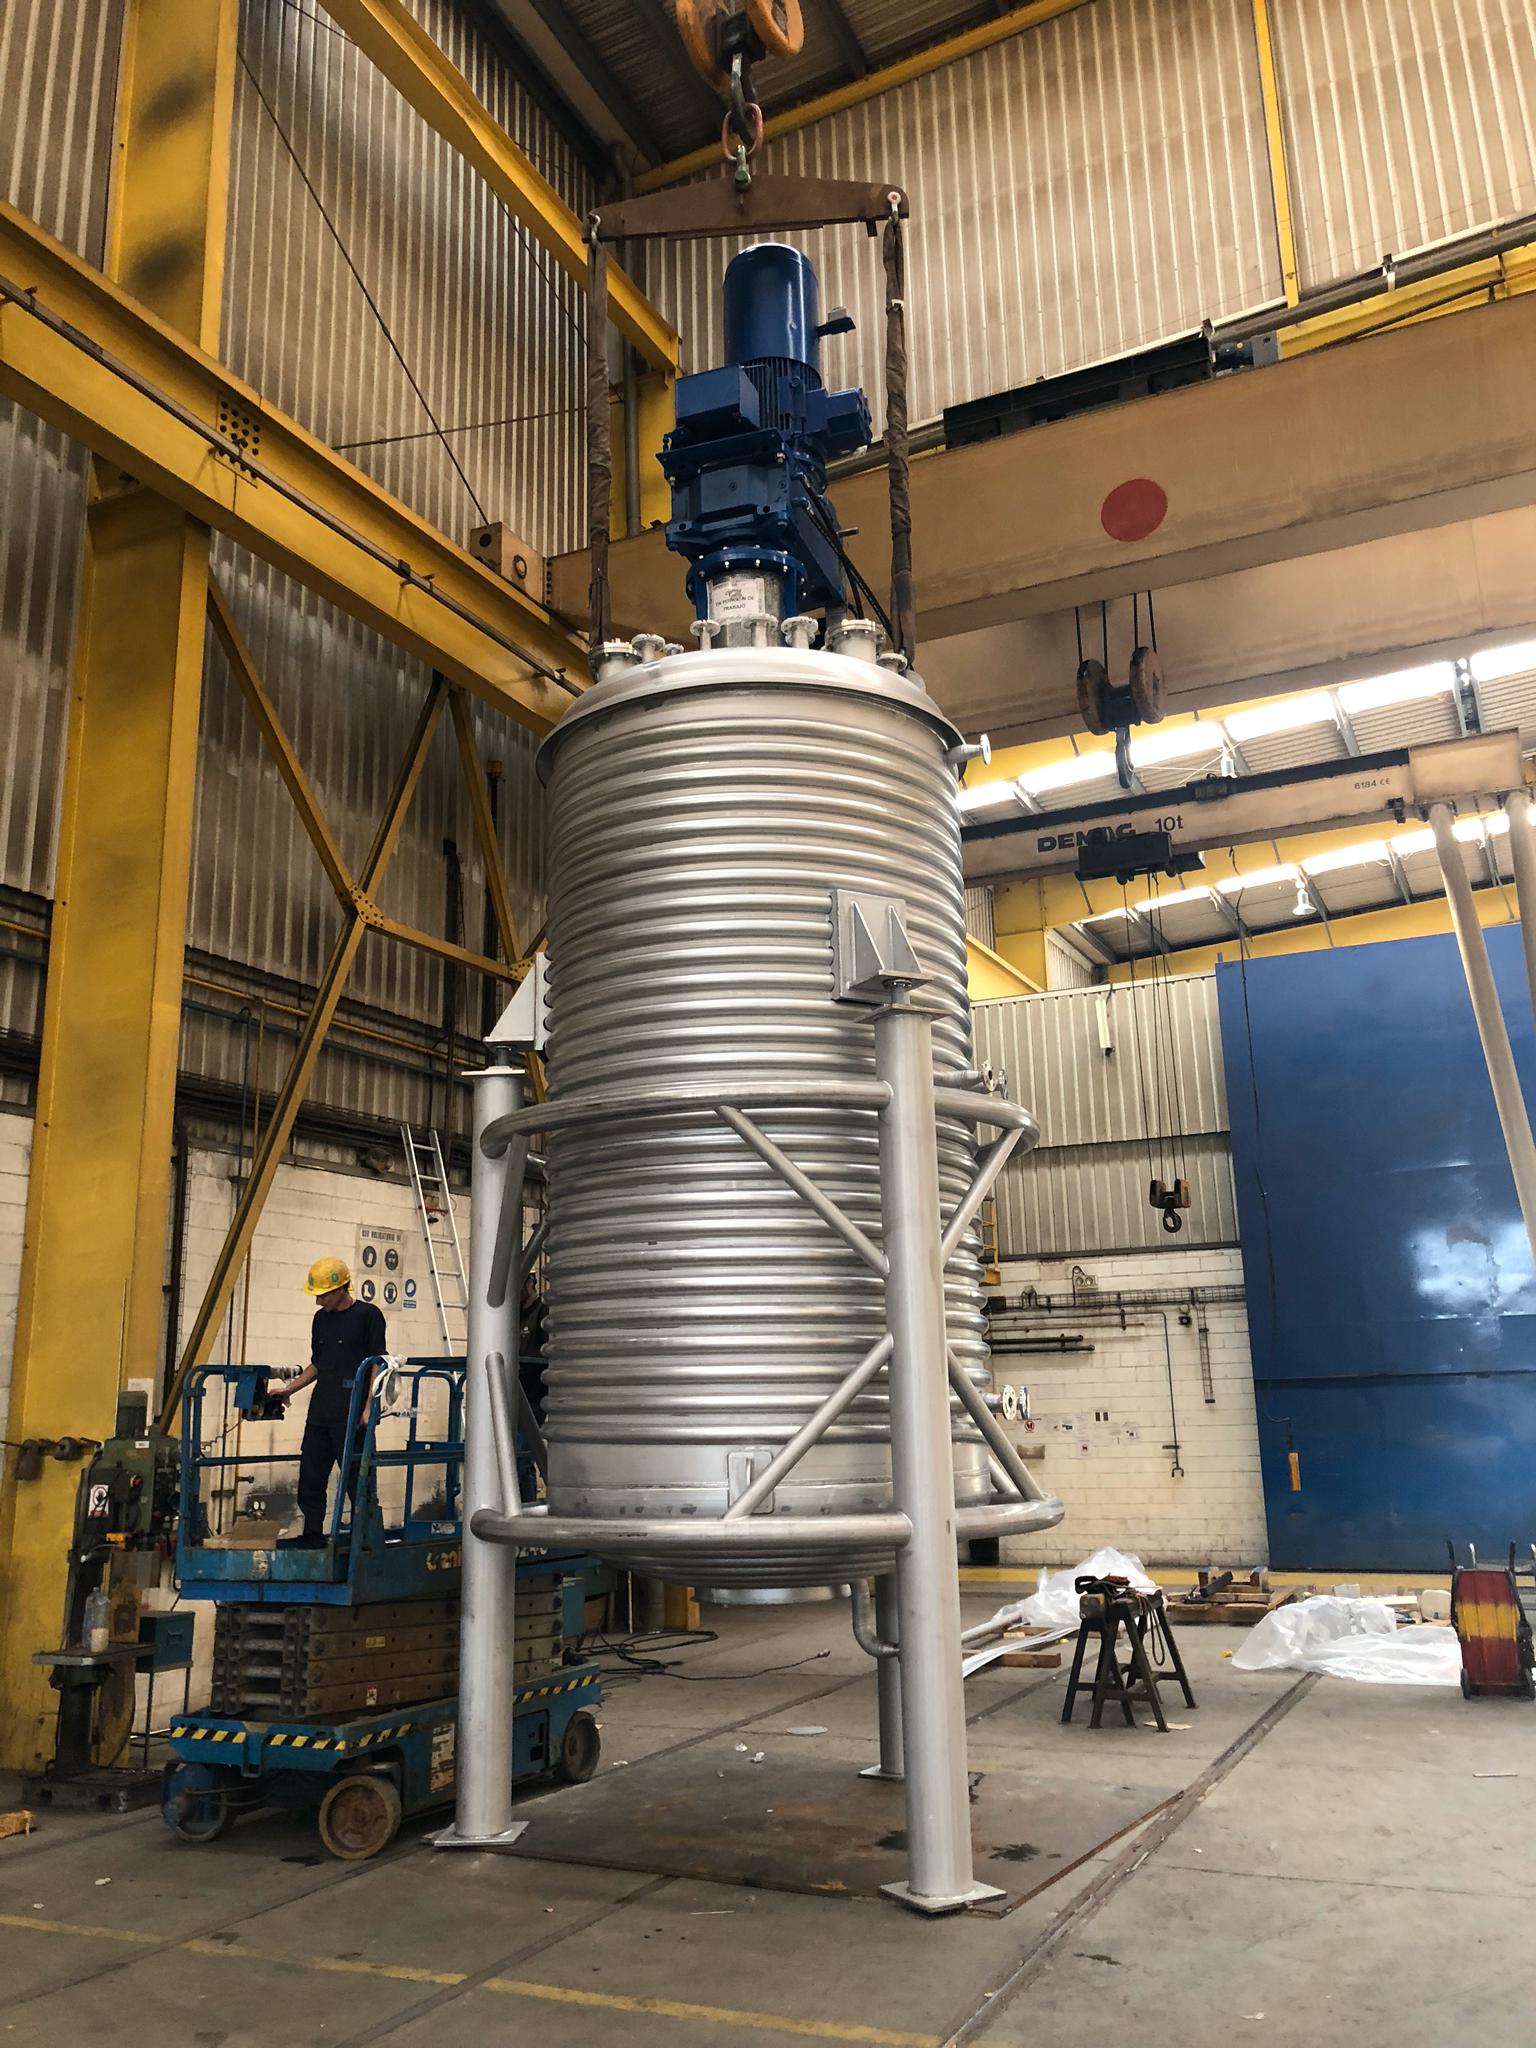
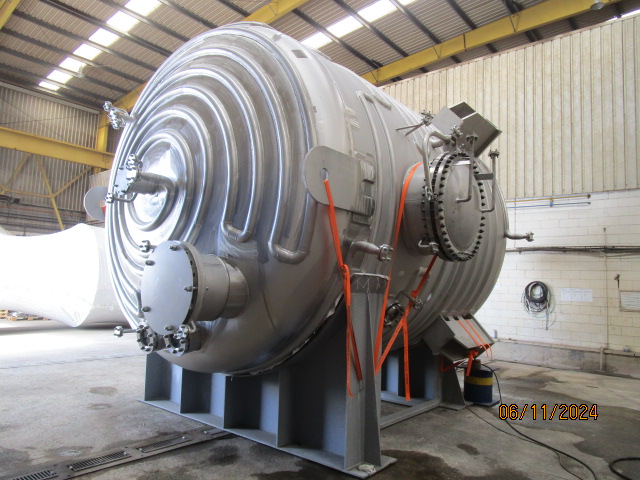
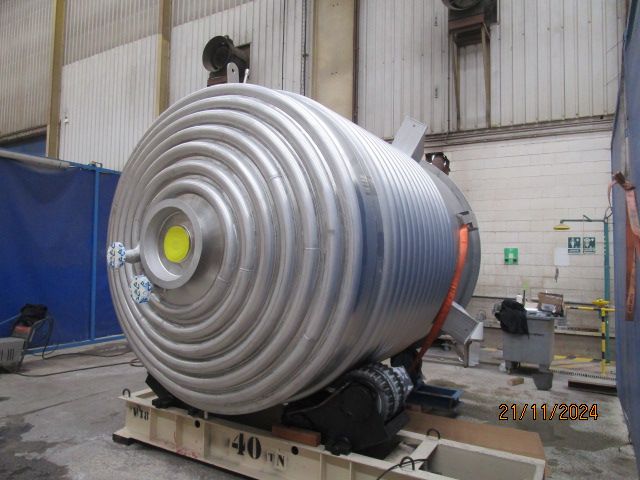
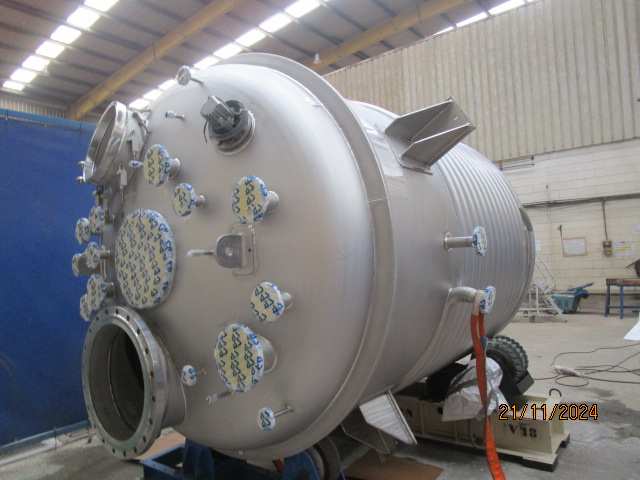
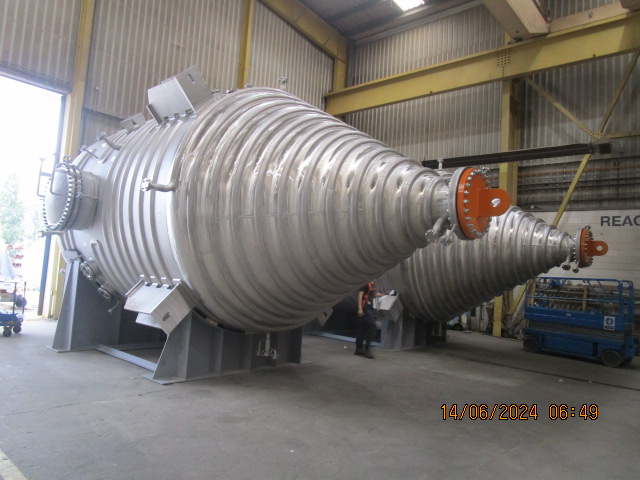
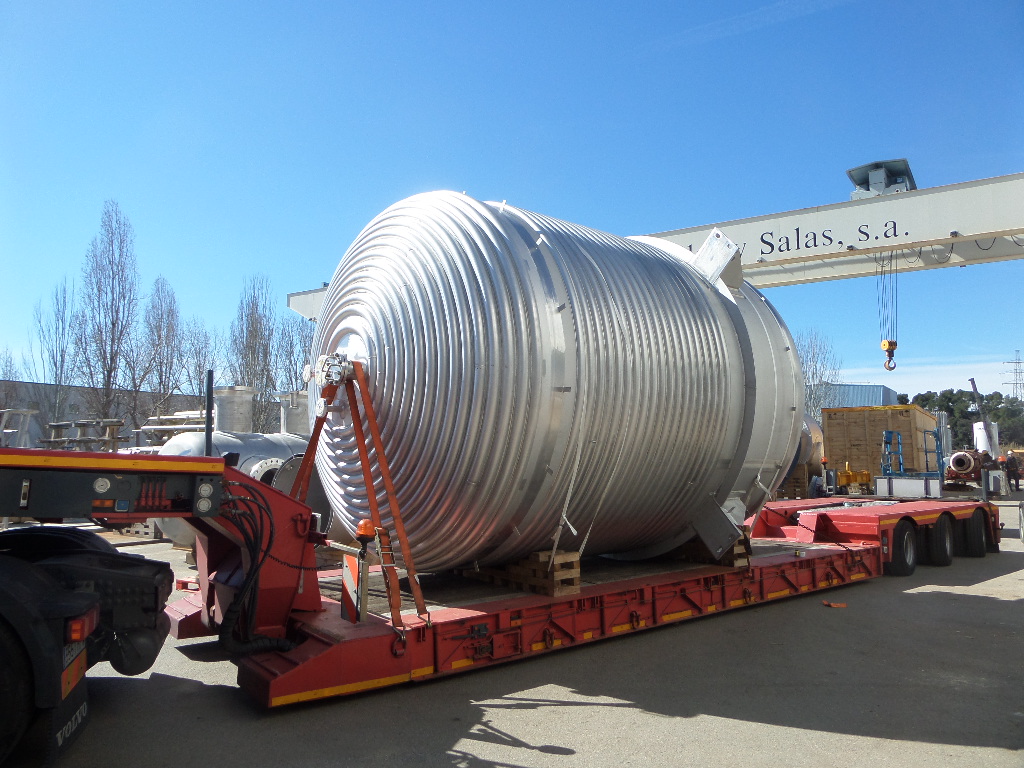
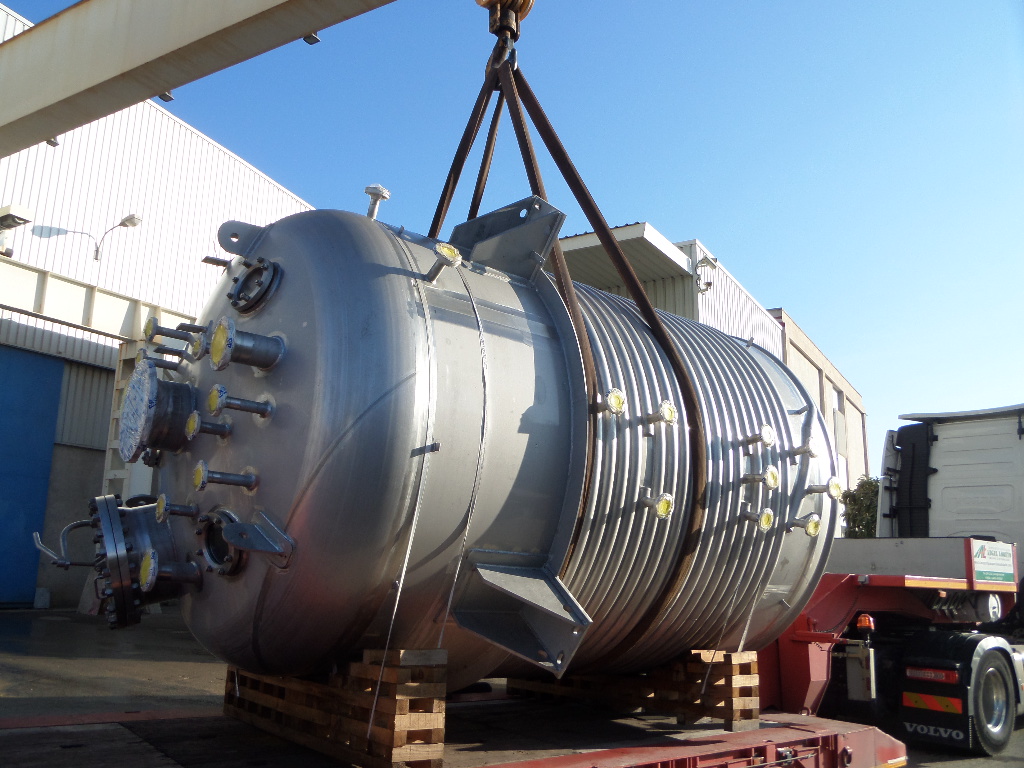
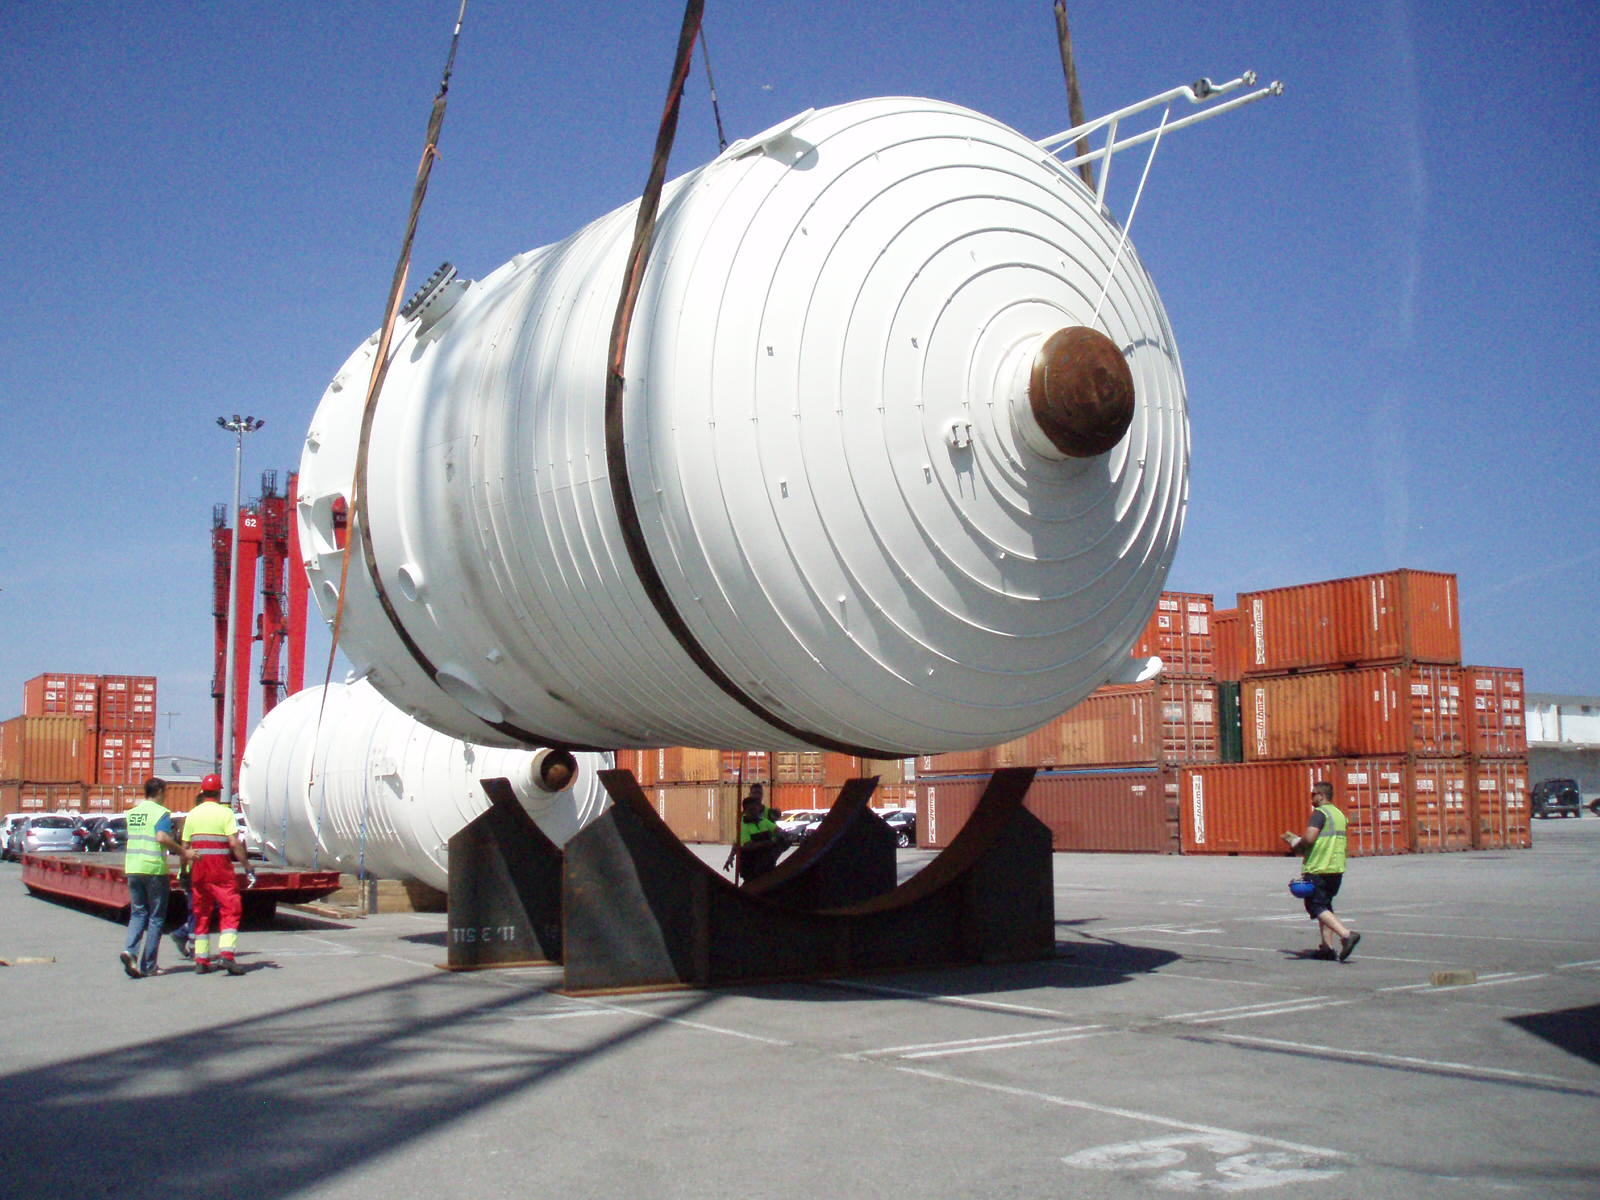
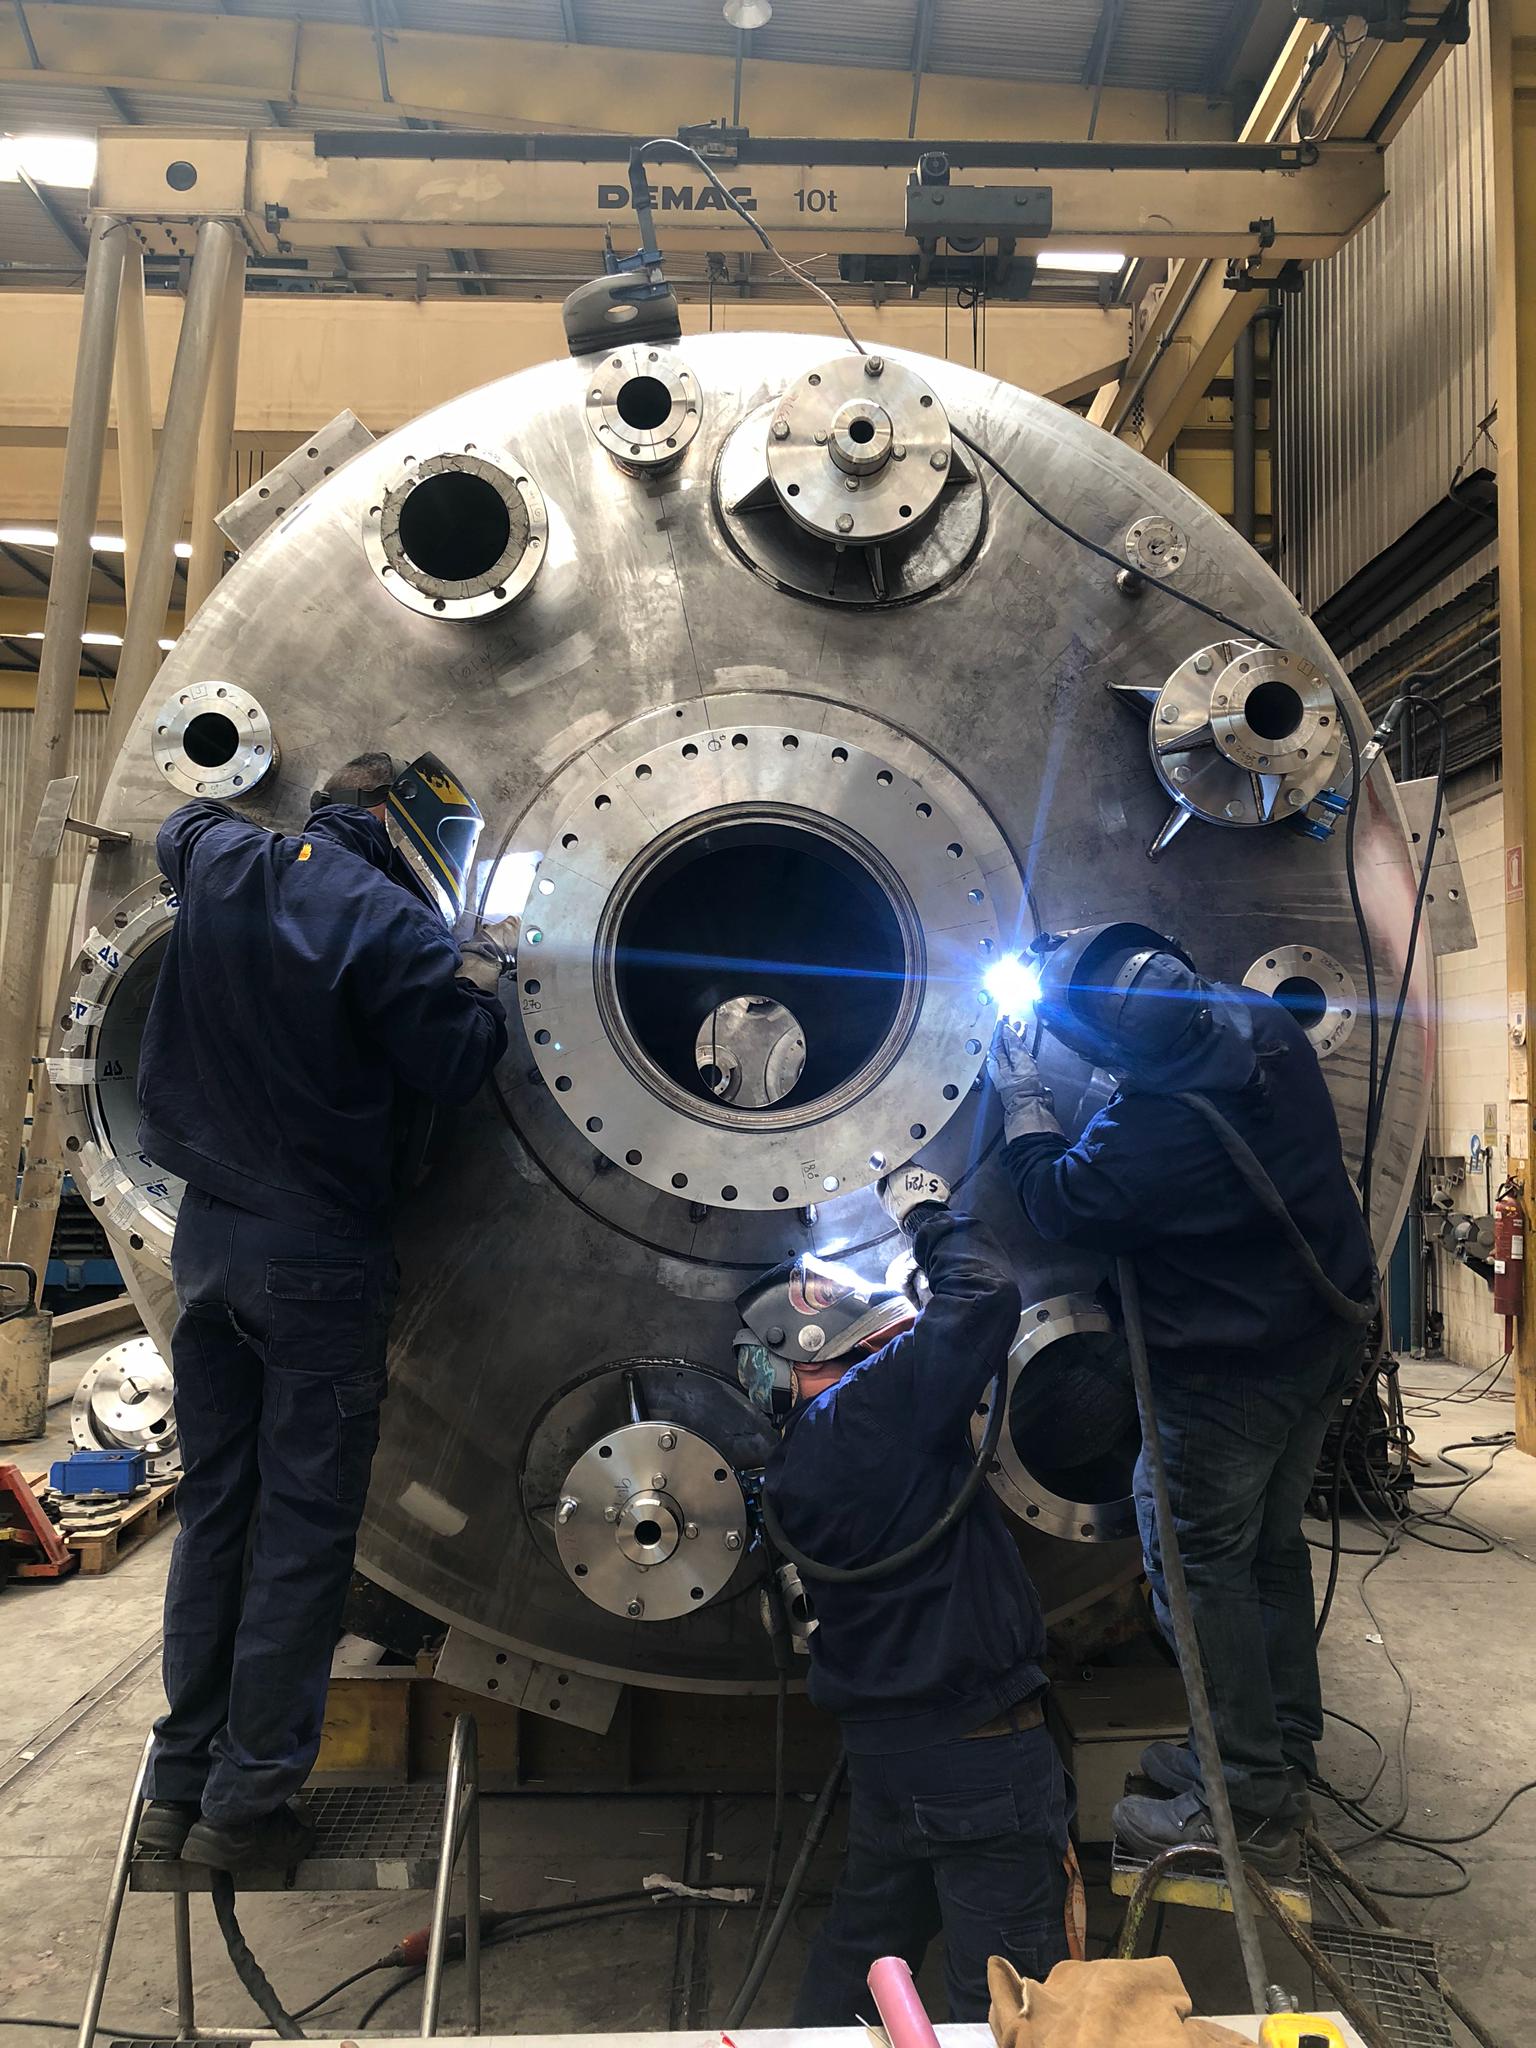
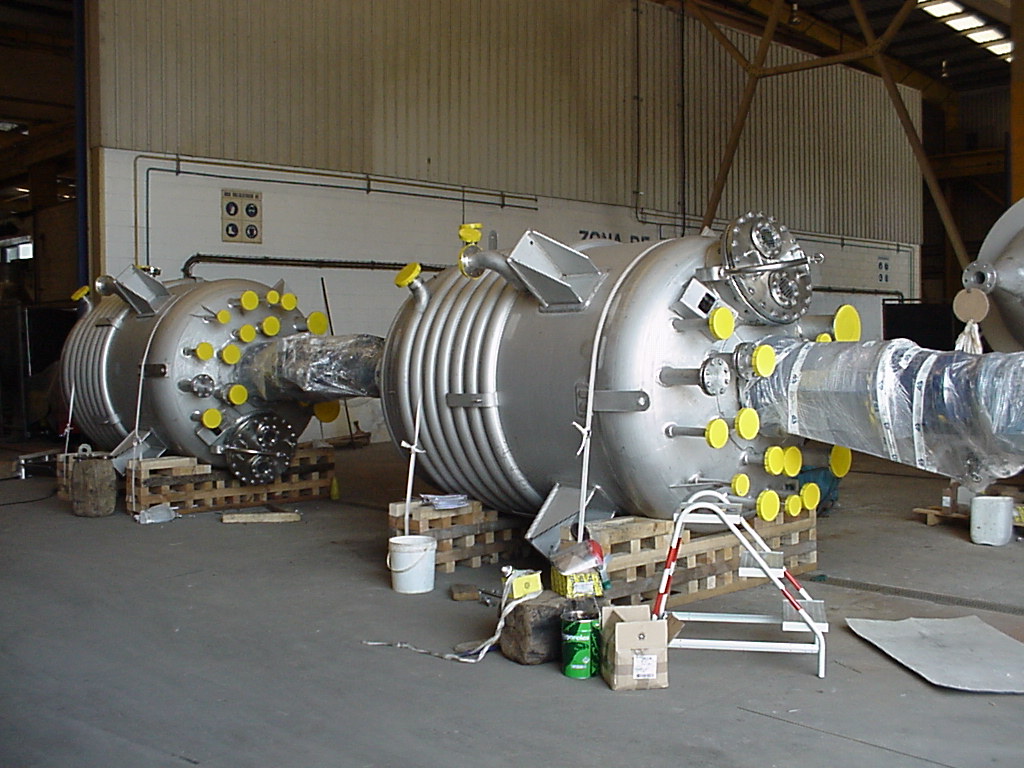
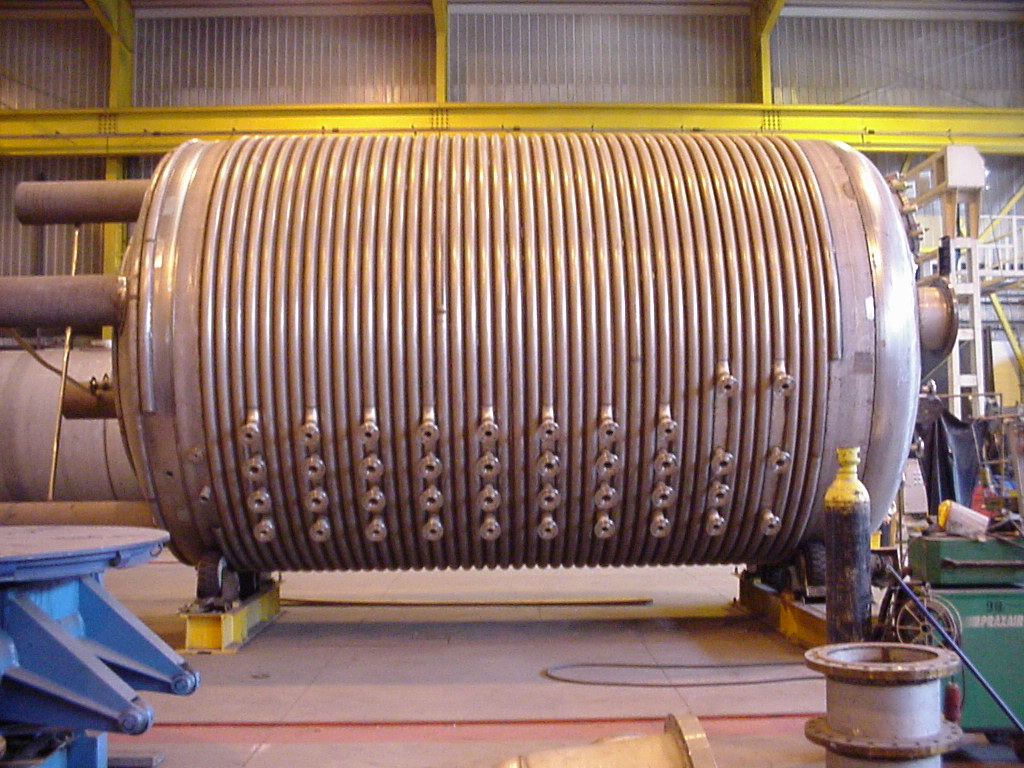
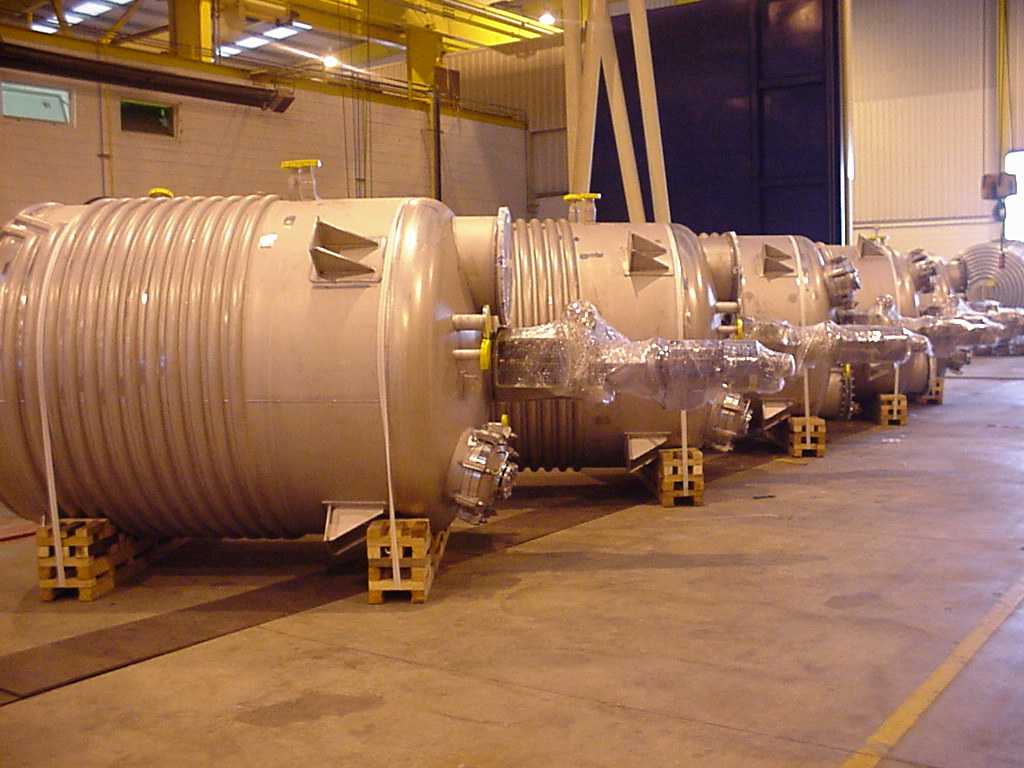
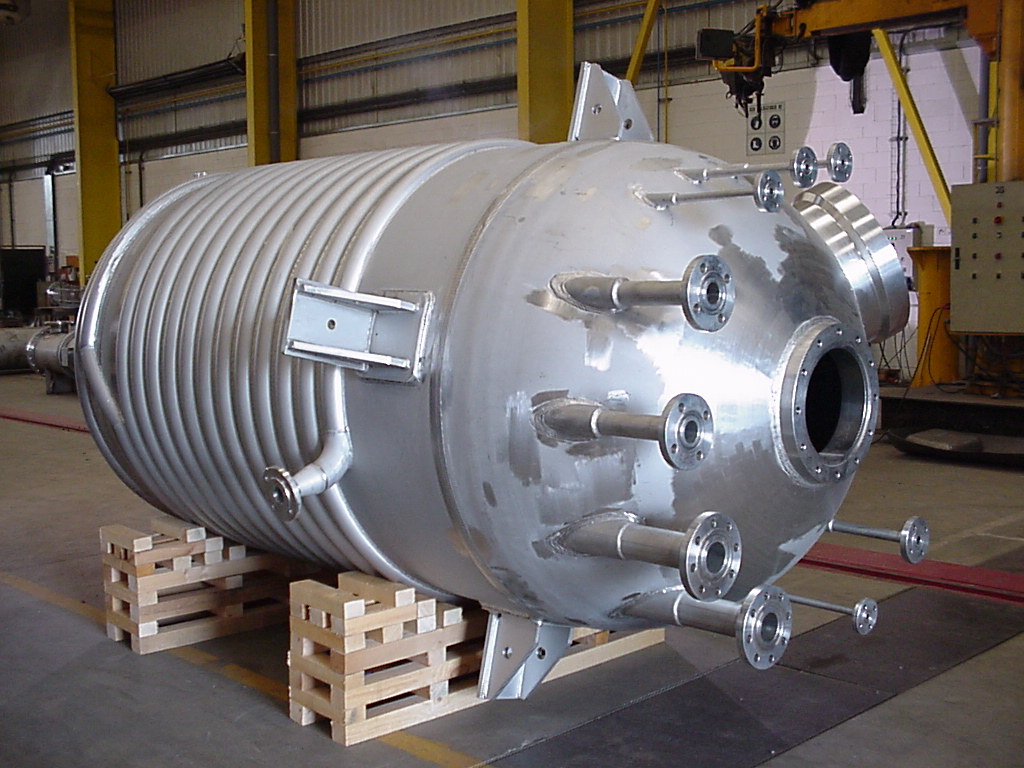
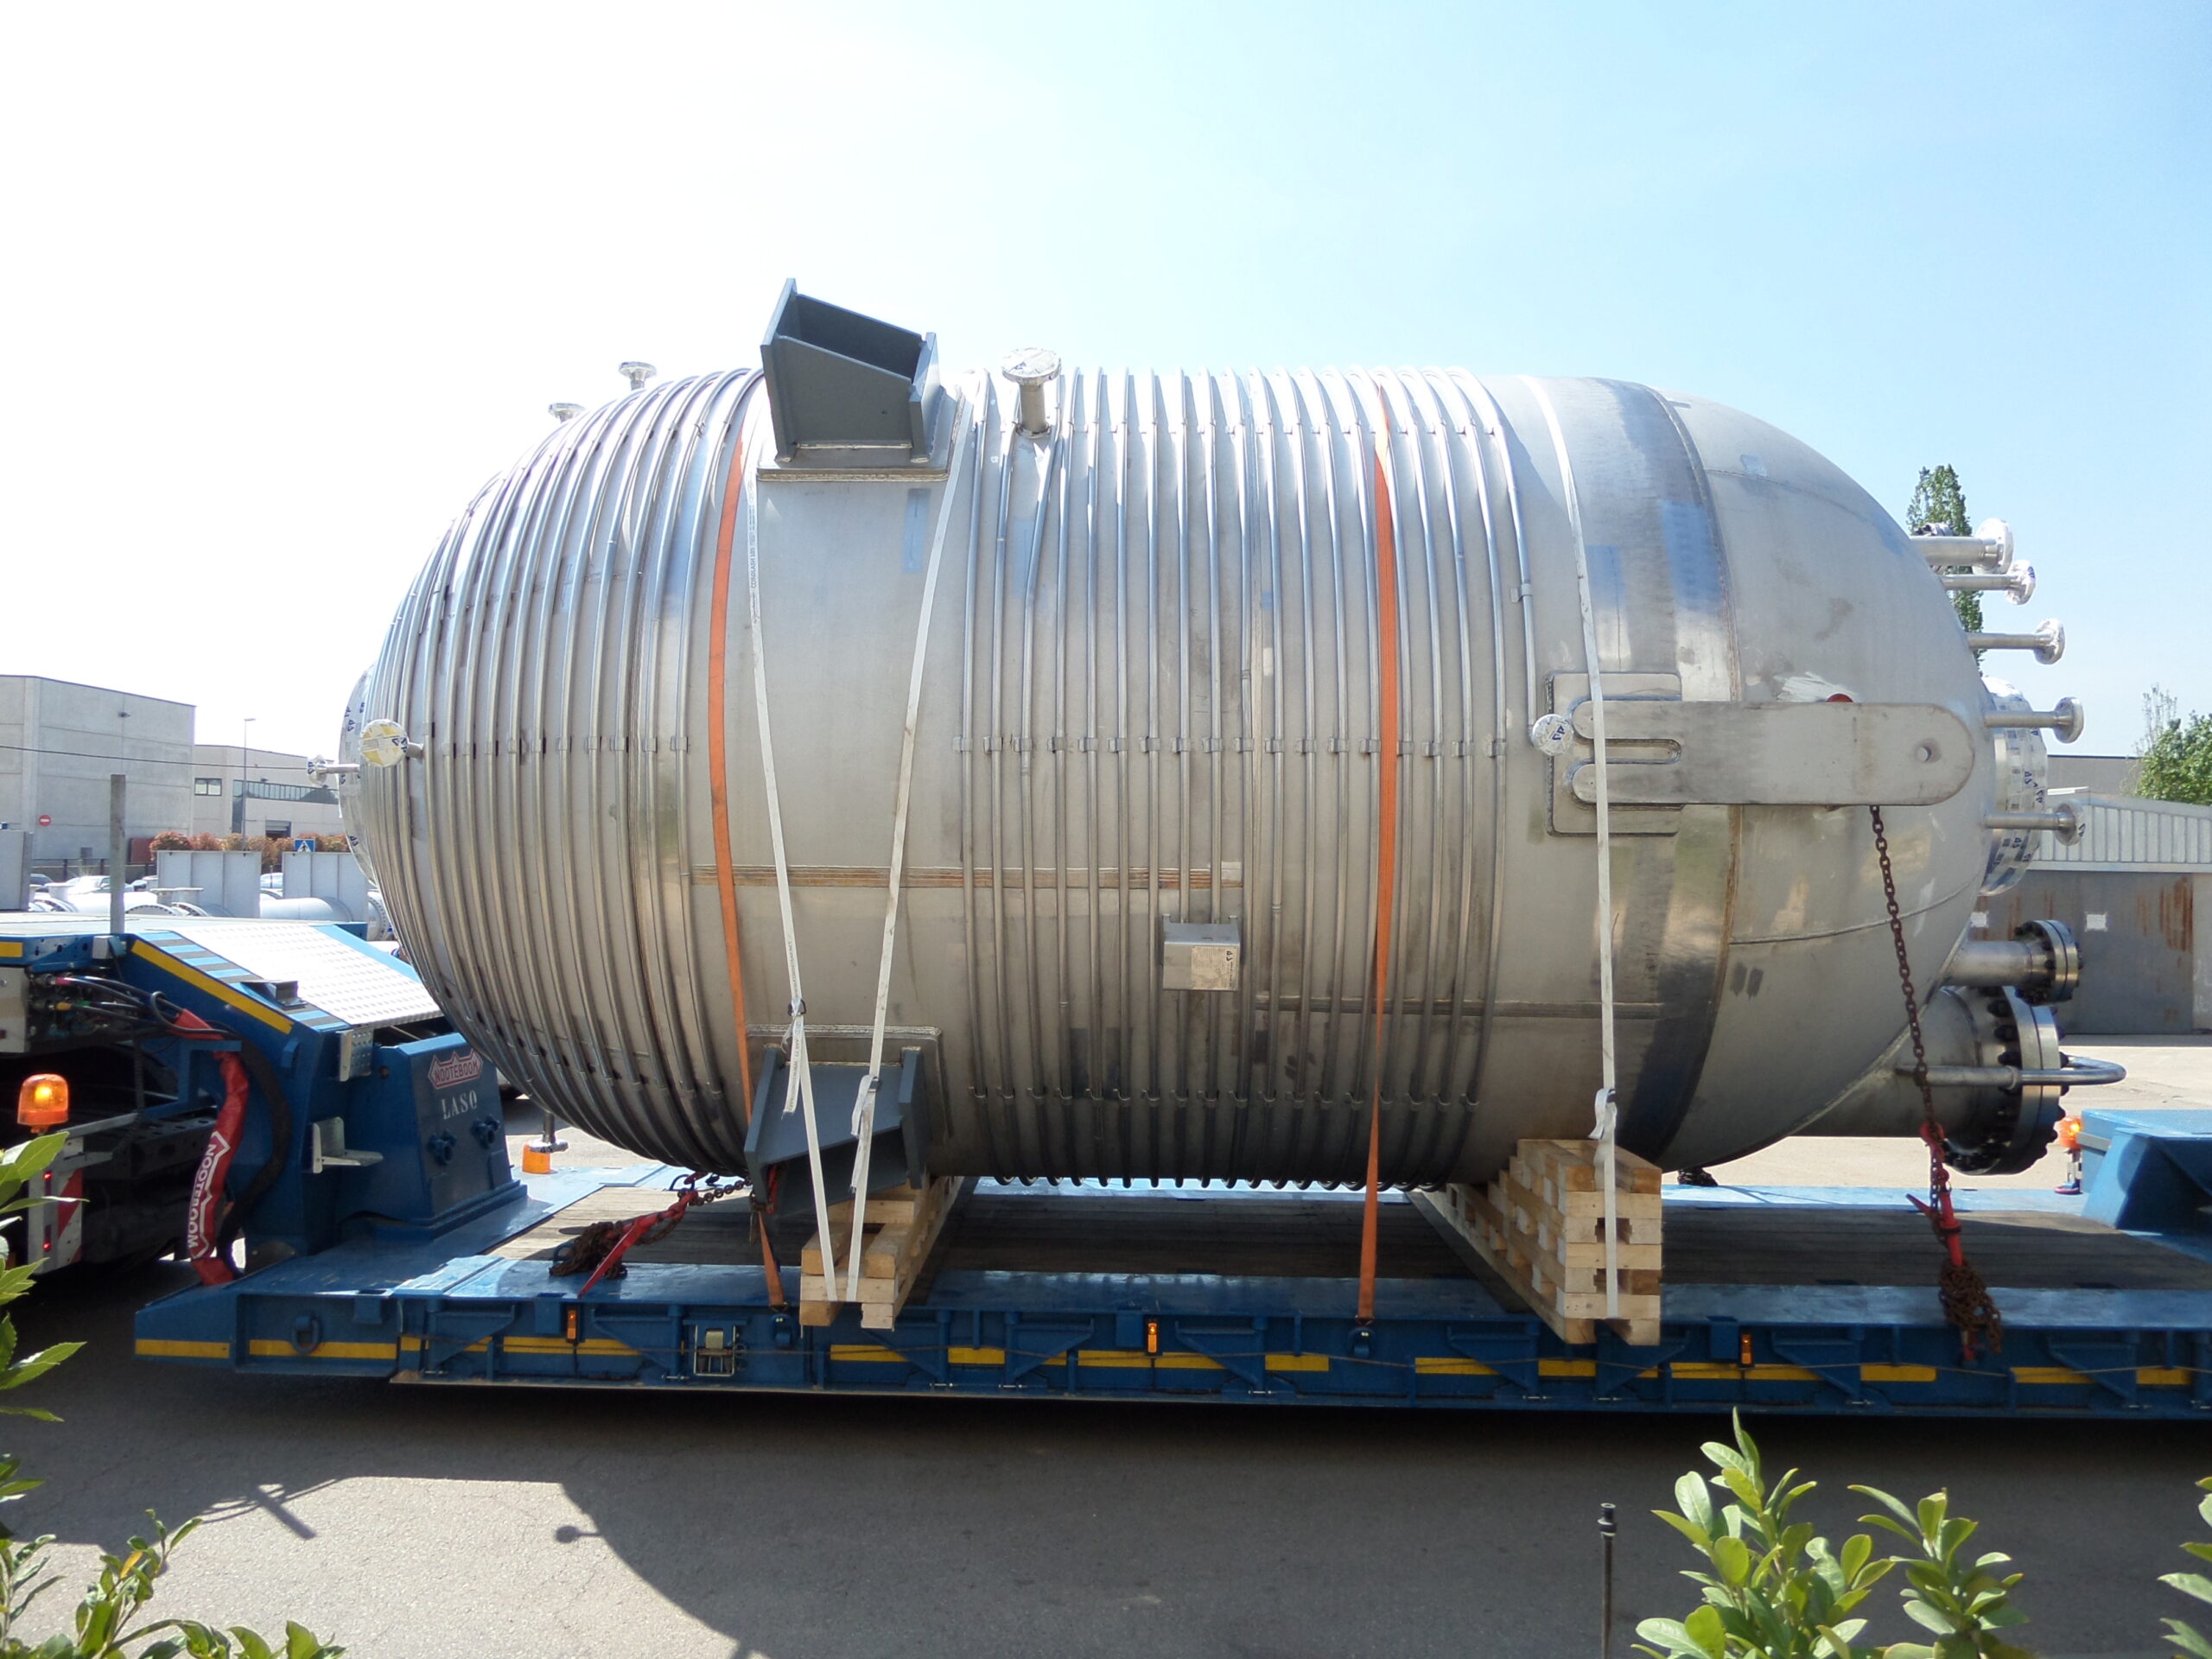
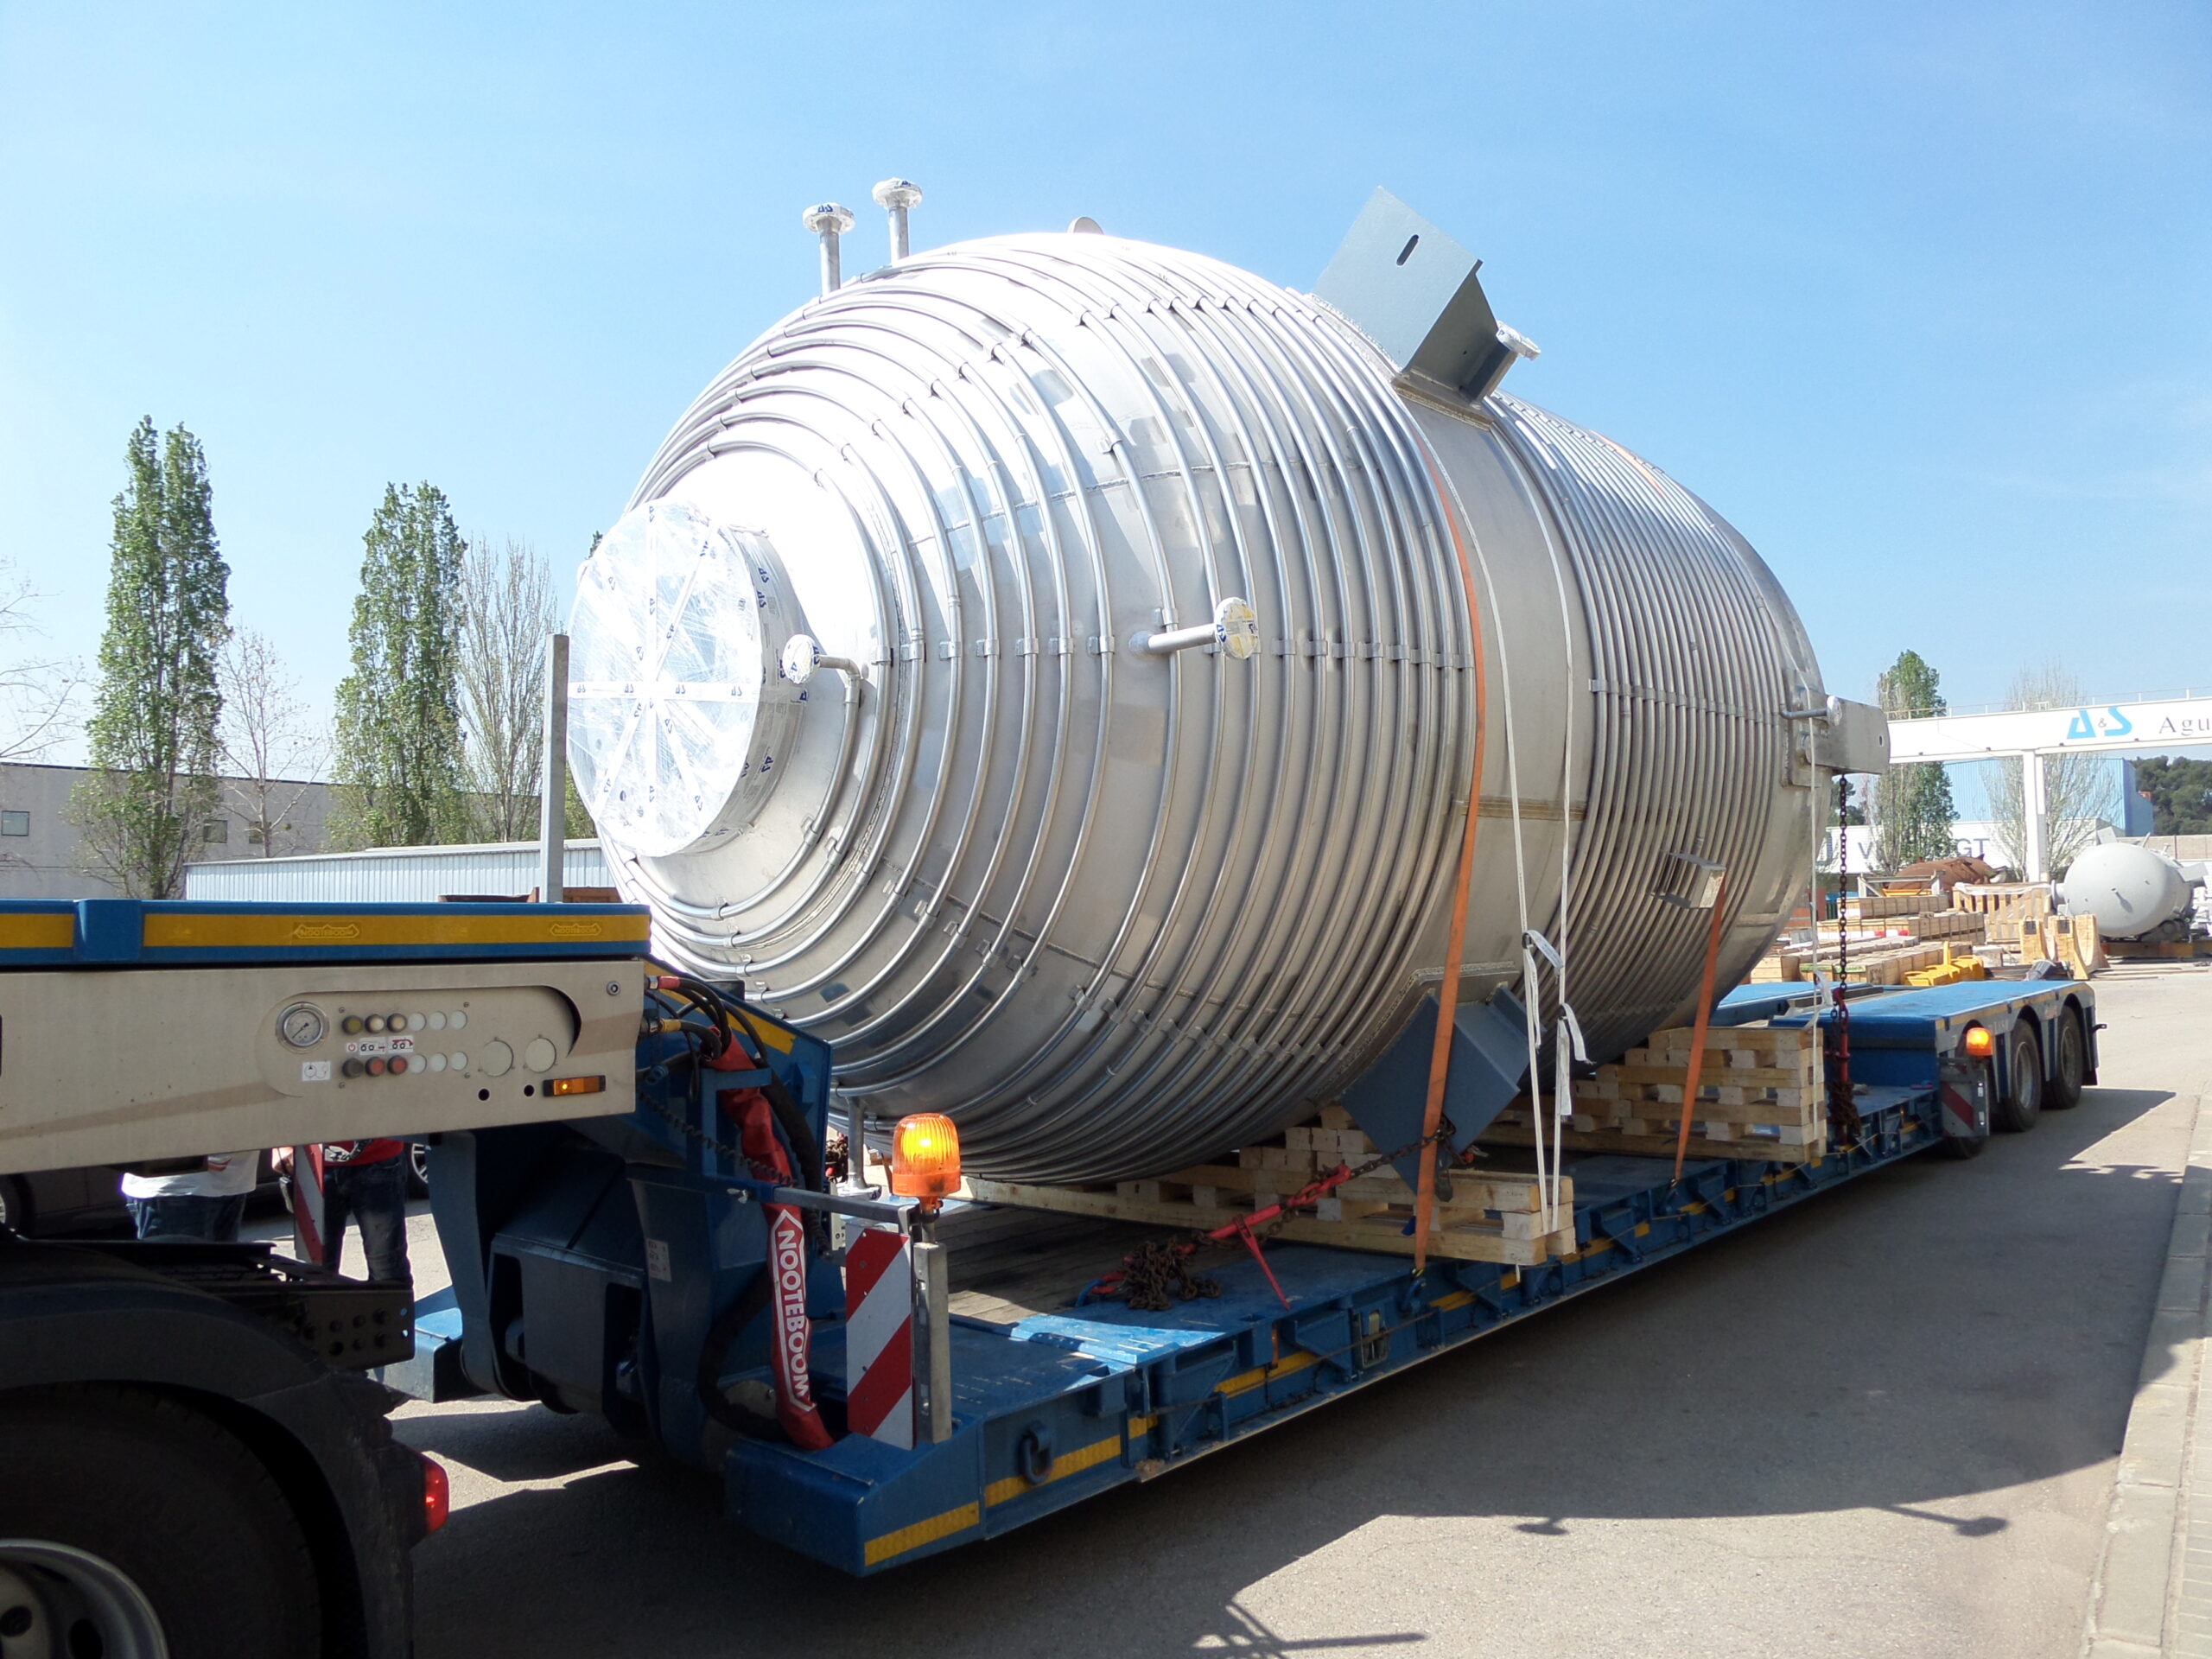
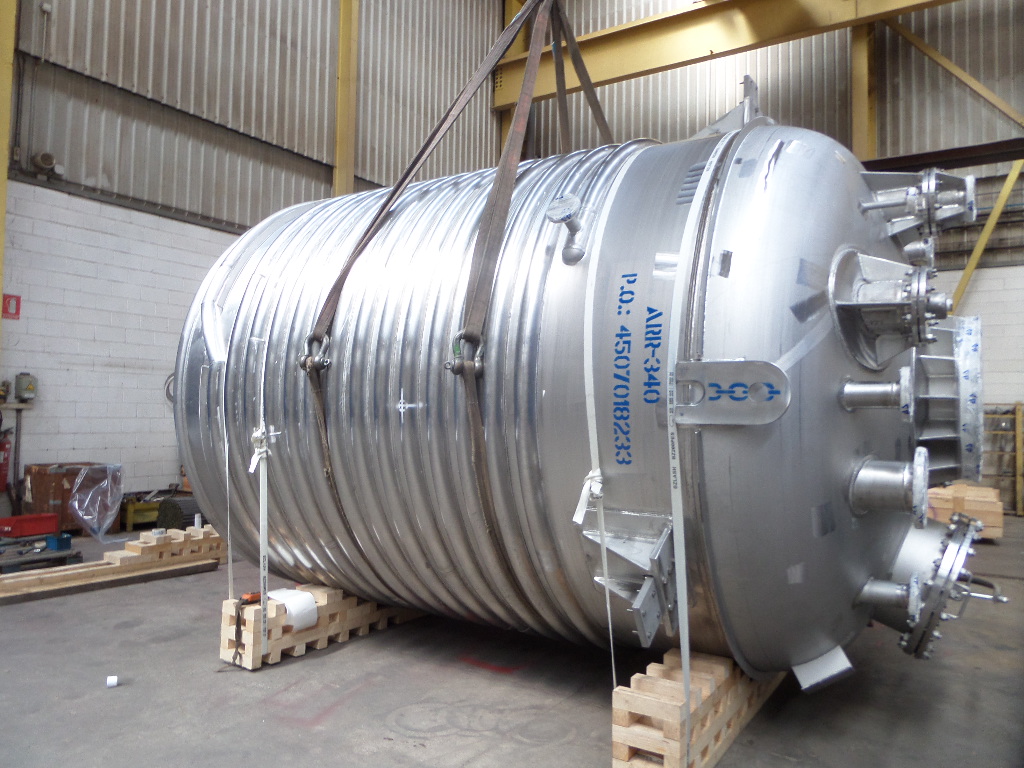
Main features of our Reactors
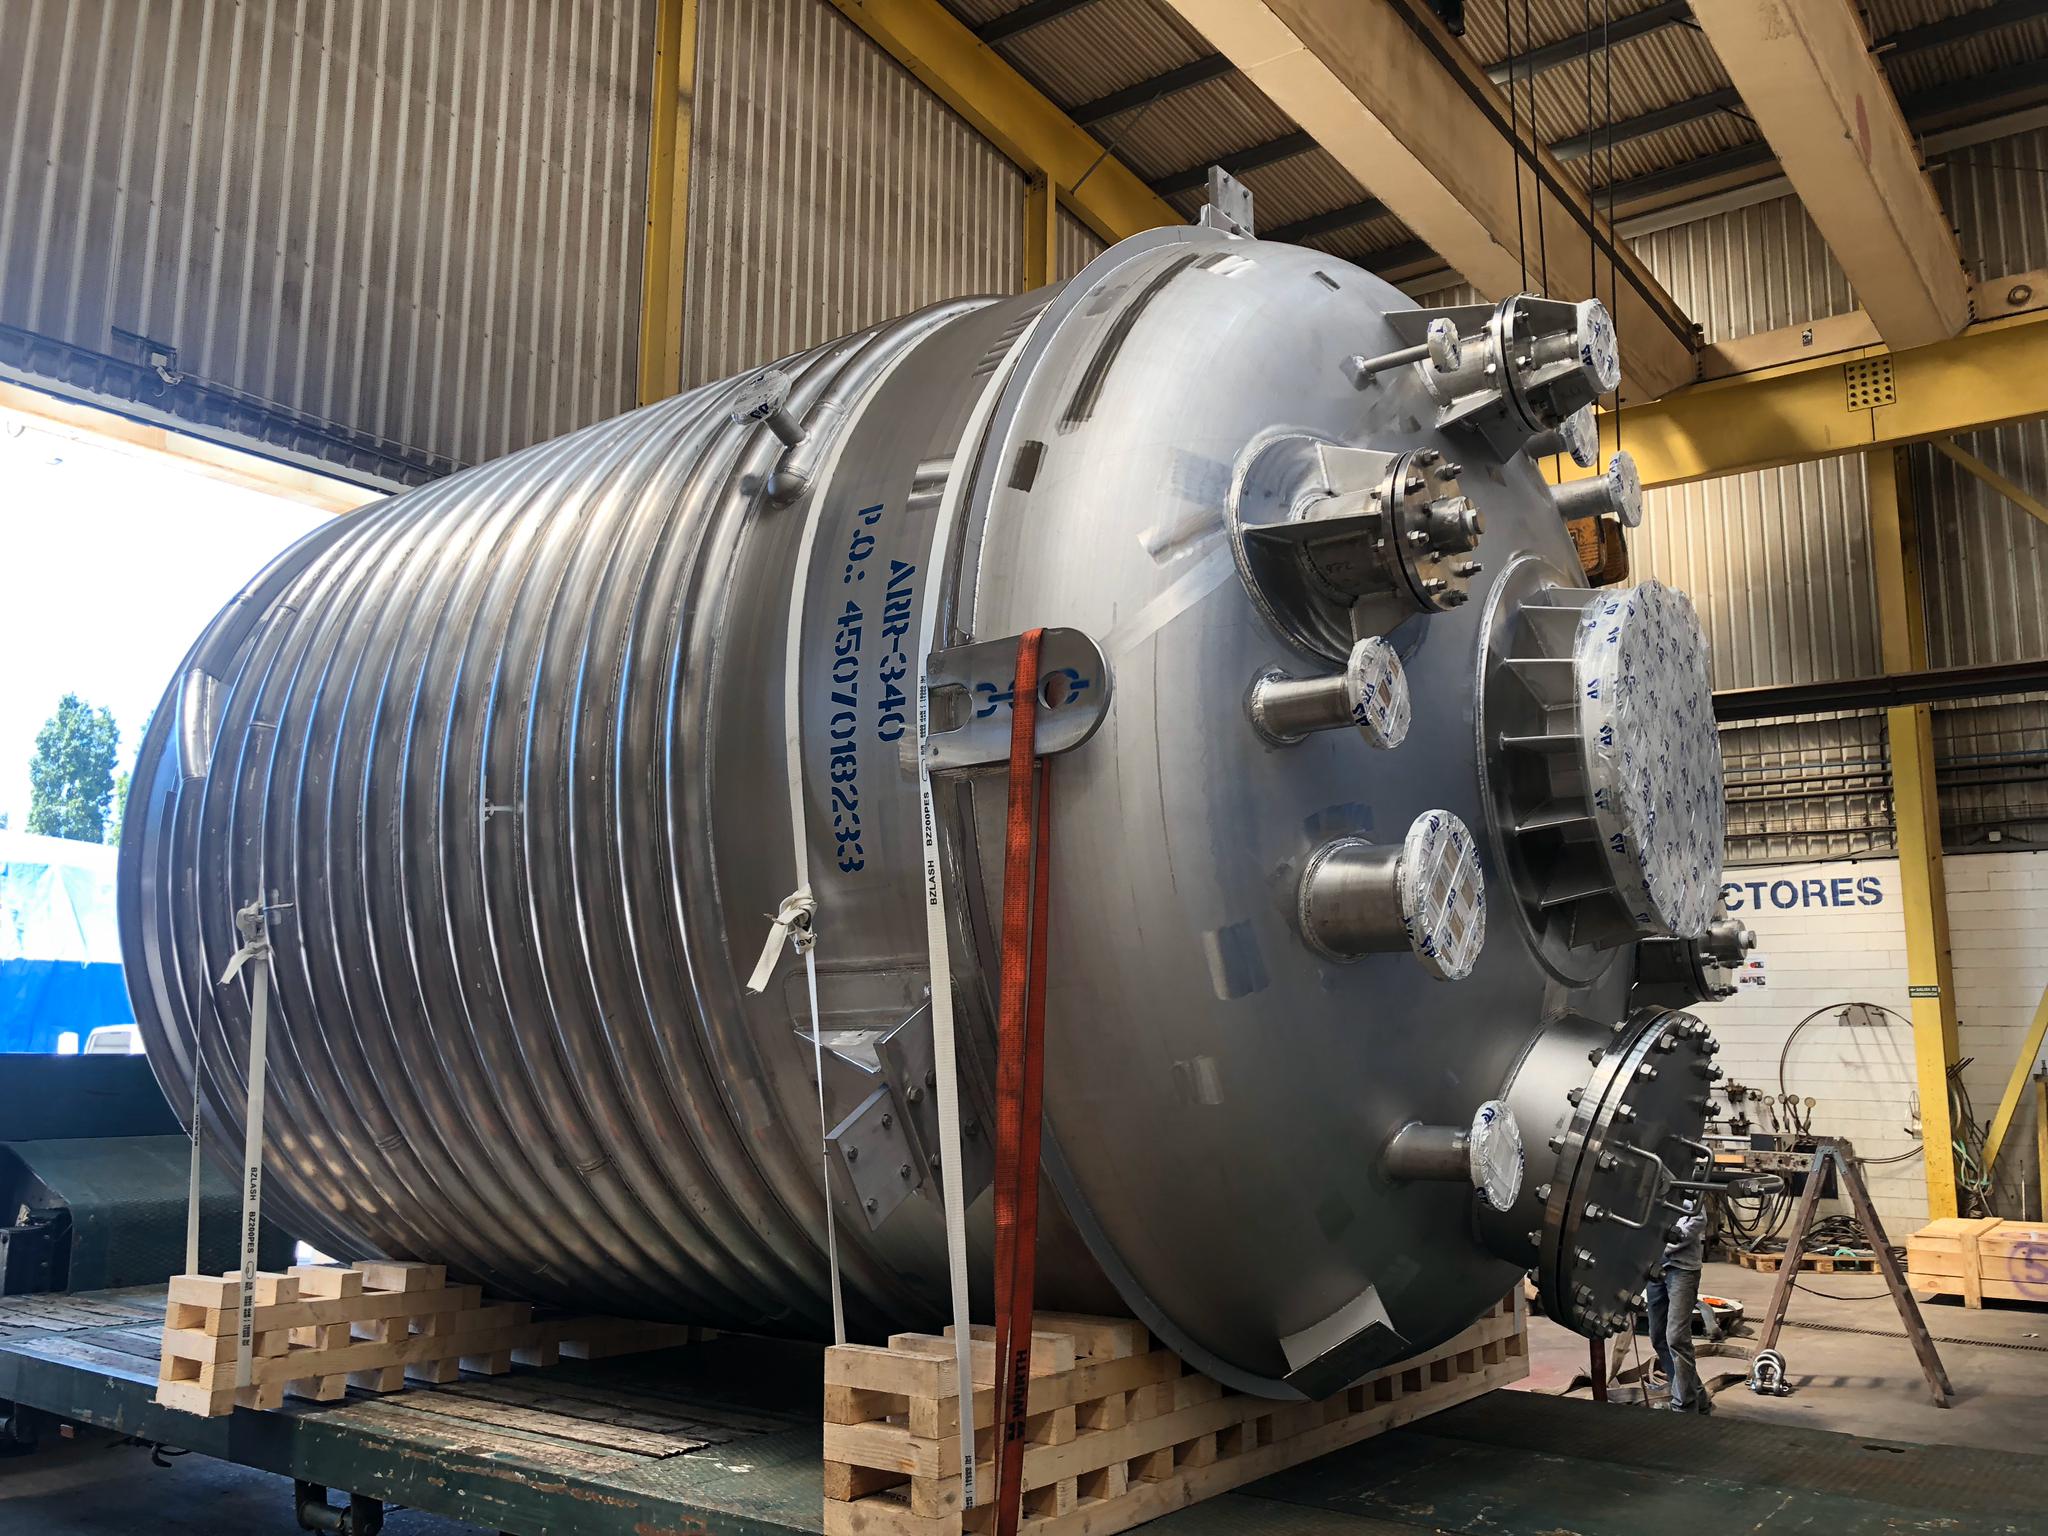
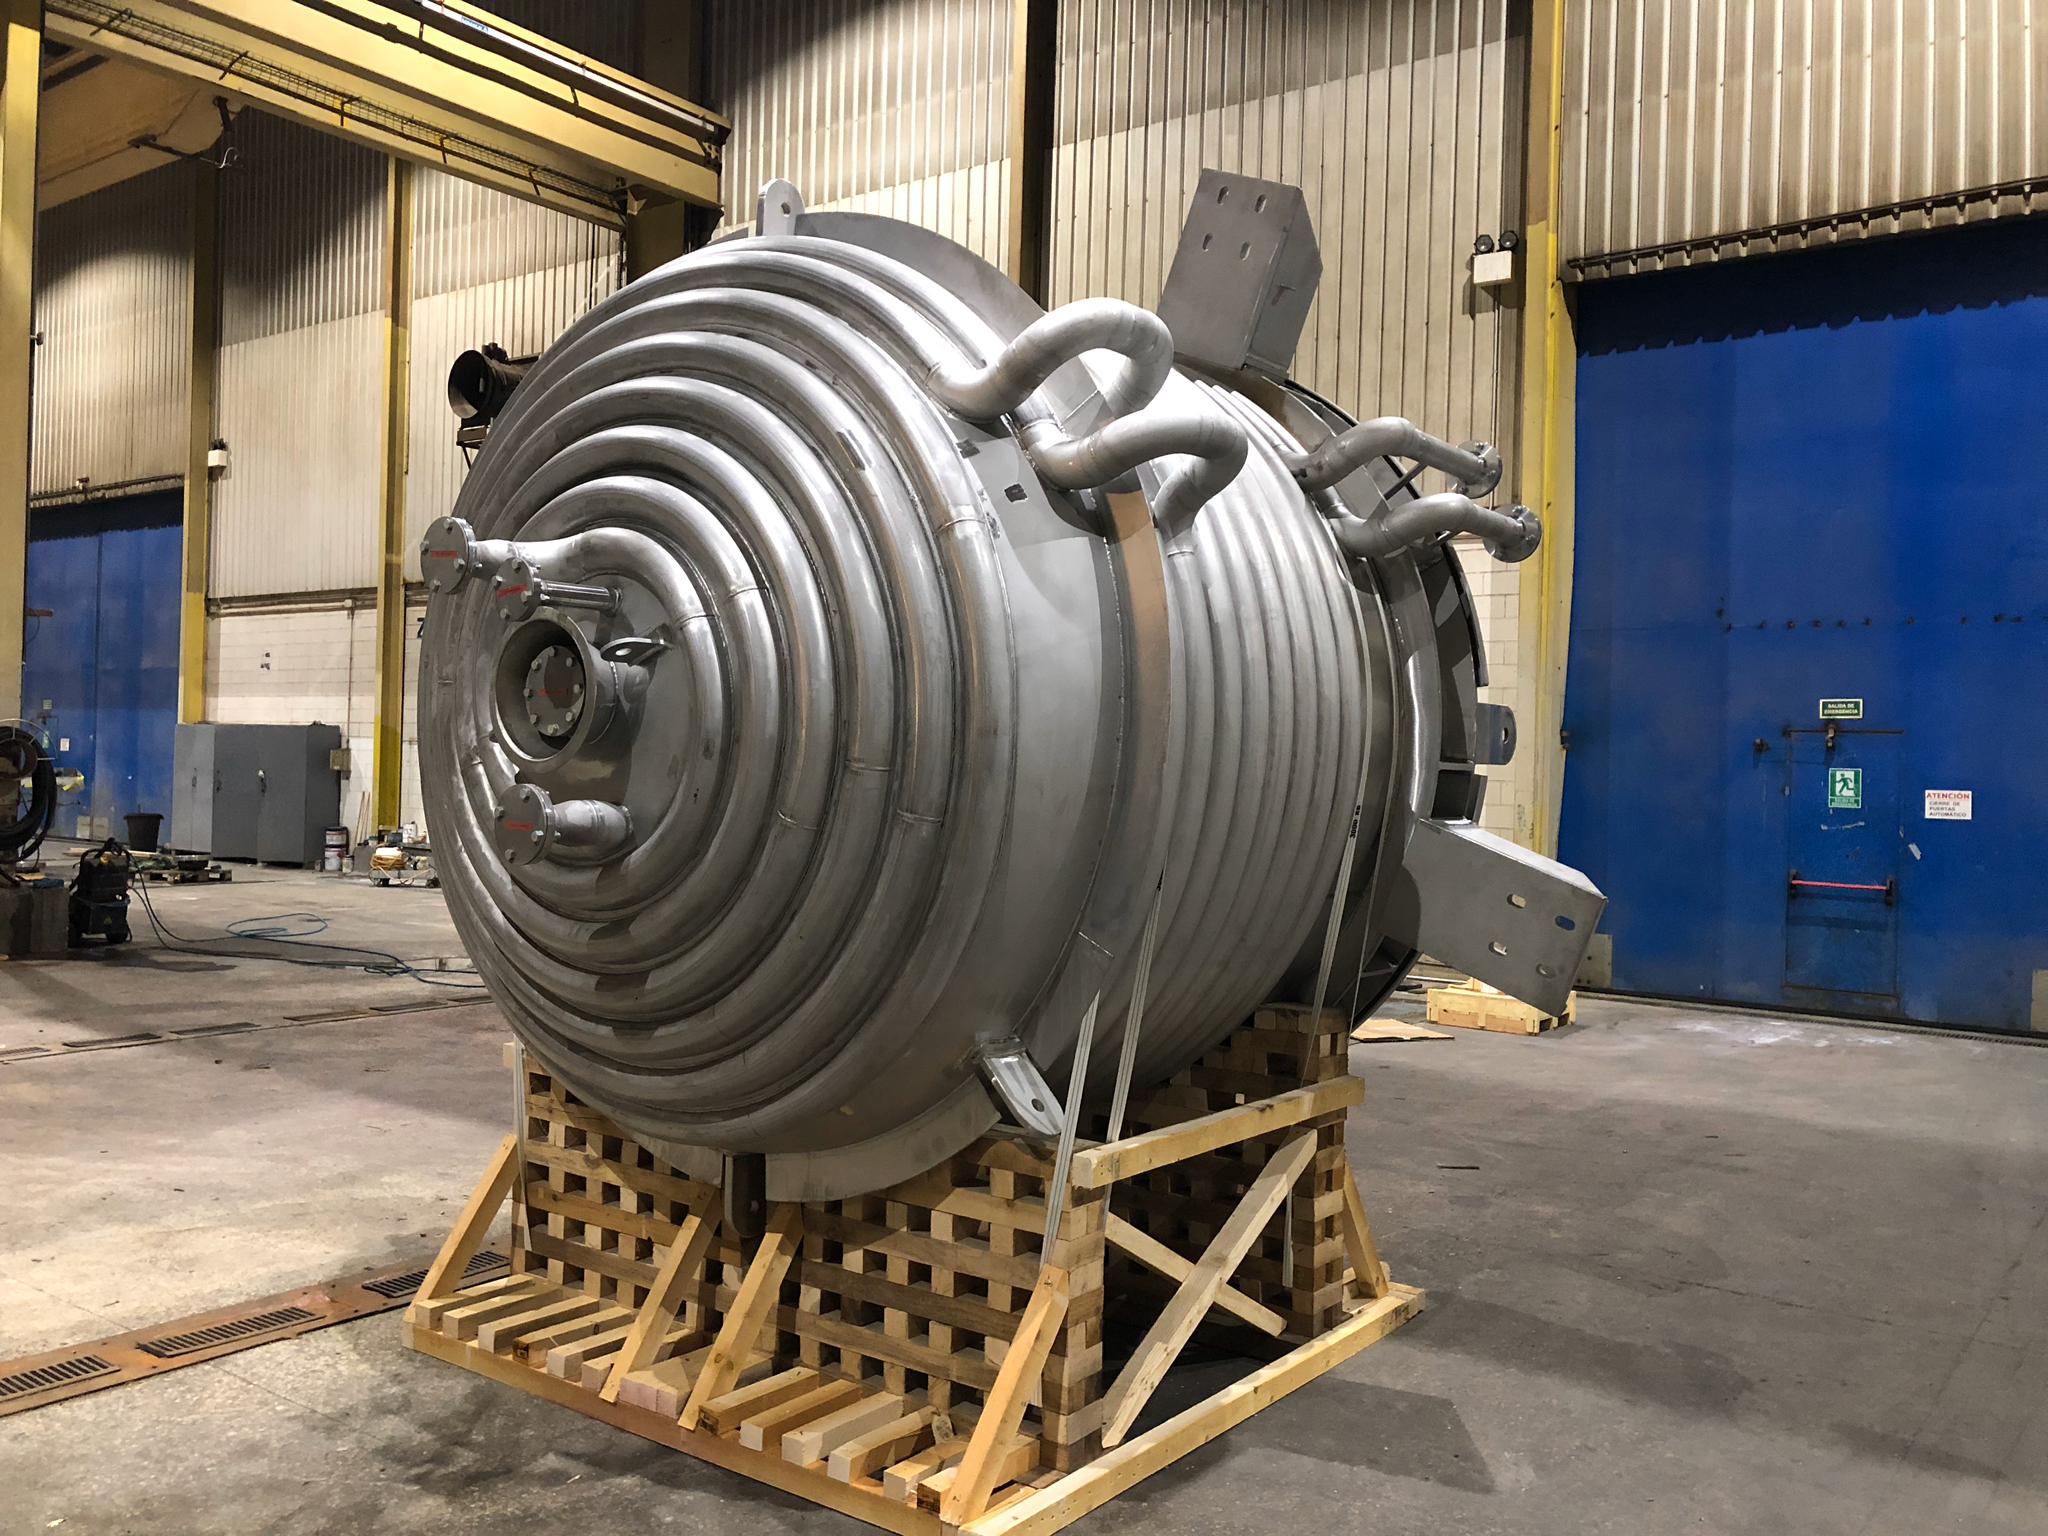
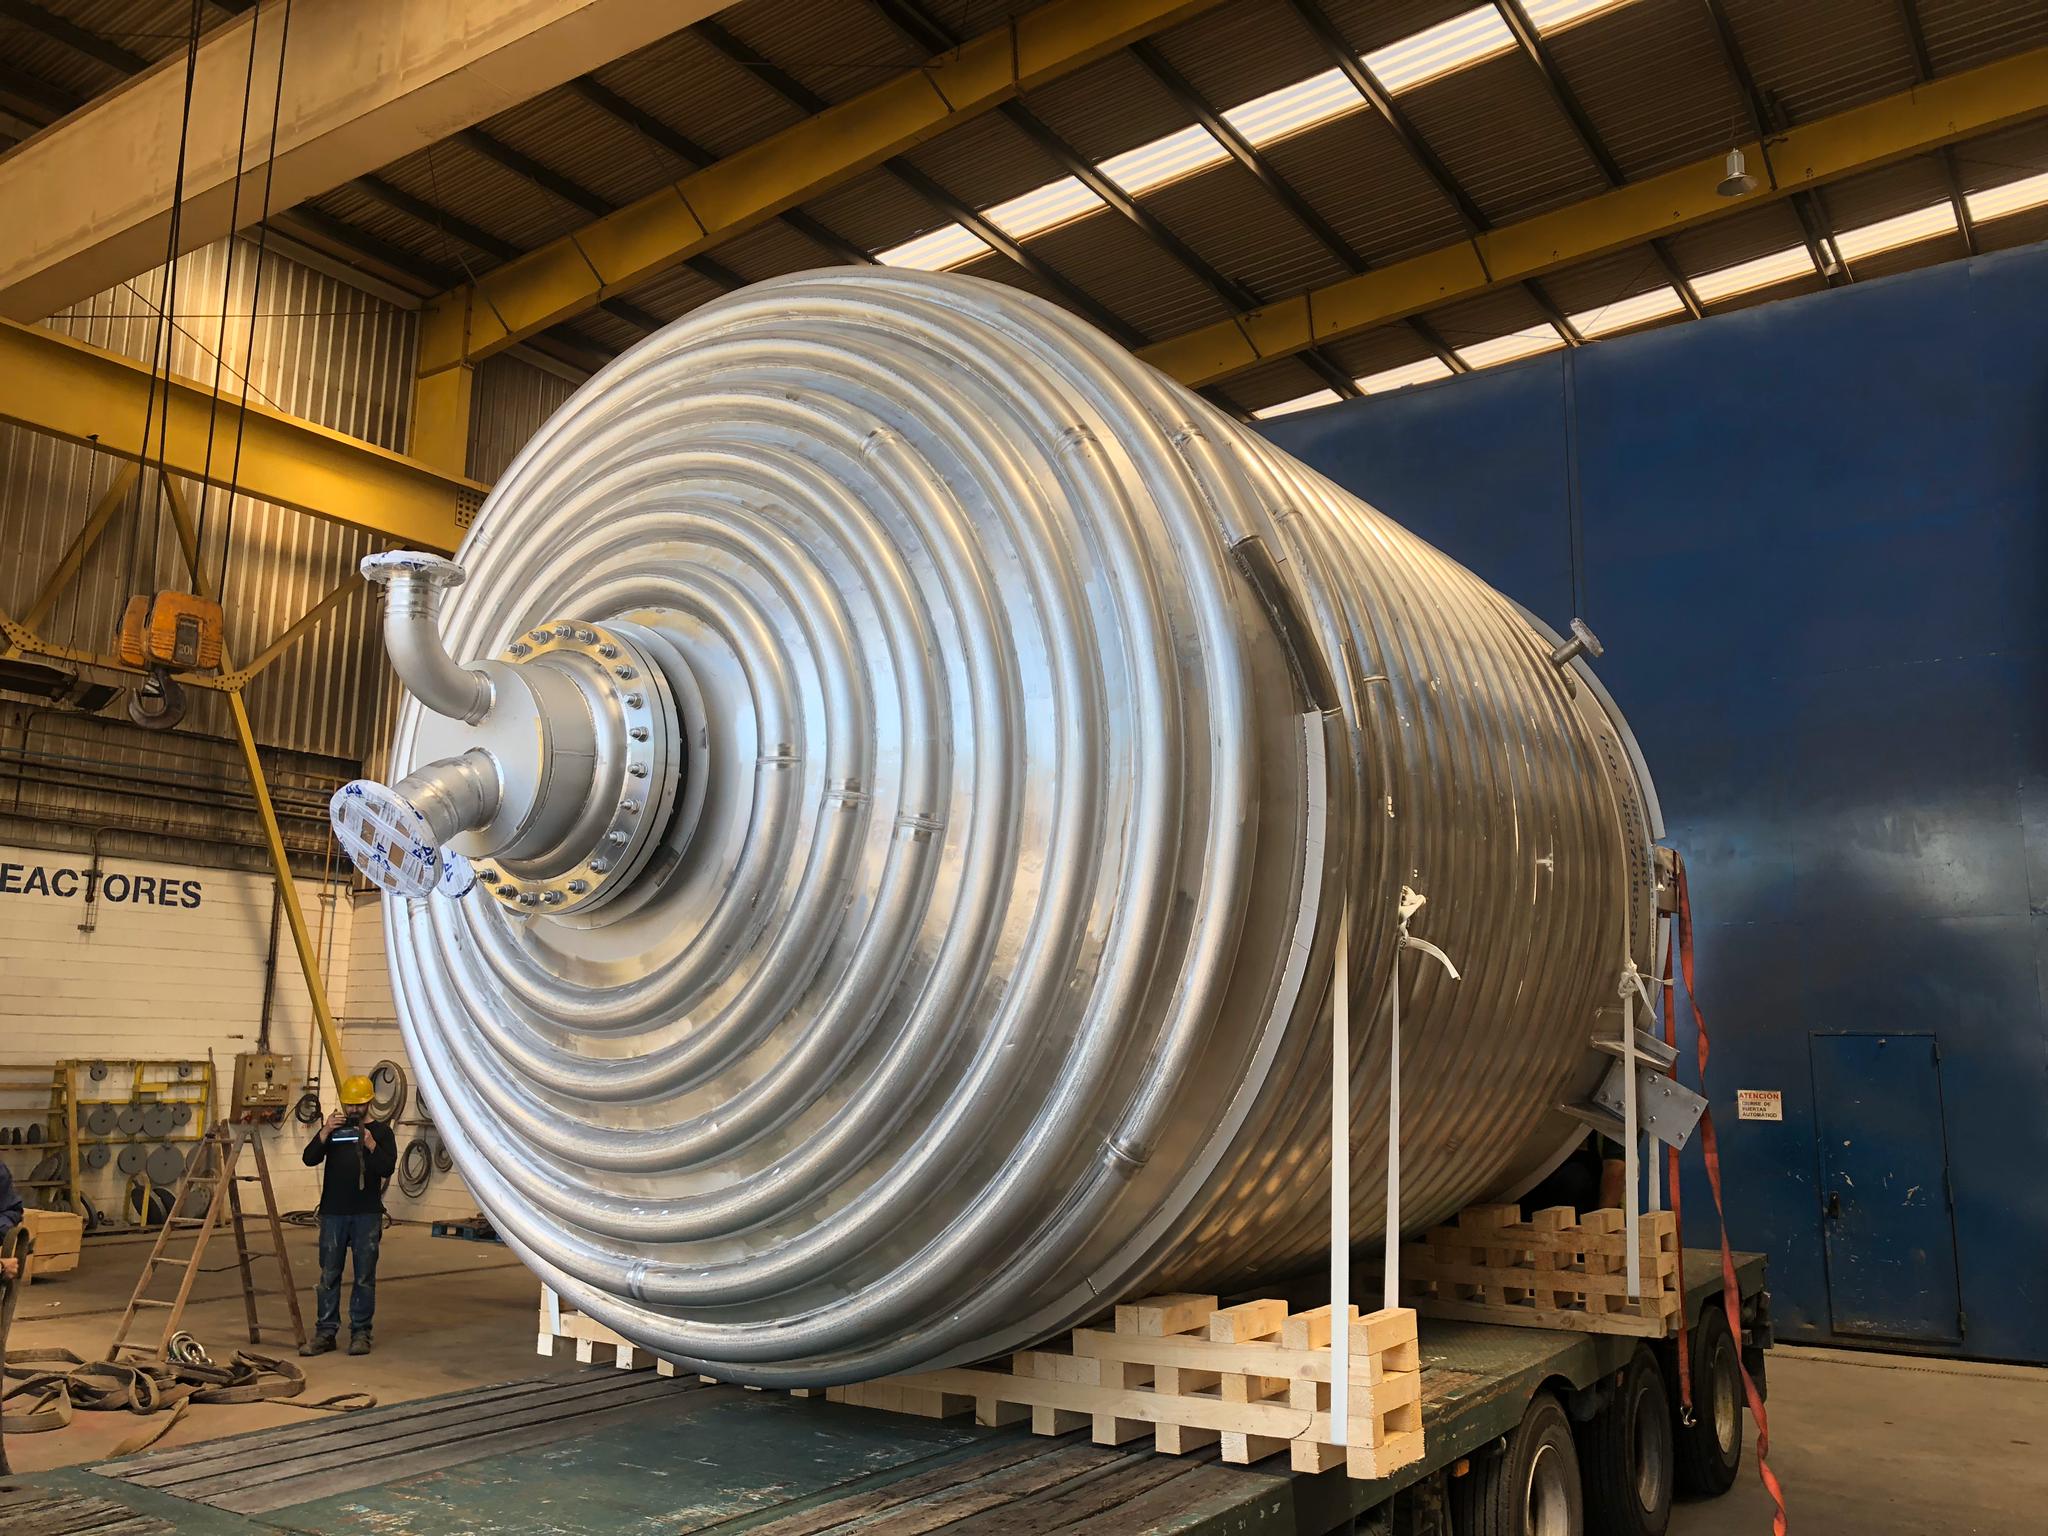
- Suitable for both low- and high-pressure reactor applications, ensuring adaptability to various operational environments.
- We manufacture reactors from a variety of materials, including stainless steel, high-nickel alloys, duplex, superduplex, cladding, and titanium, so each stainless steel reactor or titanium reactor can be matched precisely to your process chemistry.
- Insulation options for heat retention and compliance with ATEX standards for safety in explosive environments.
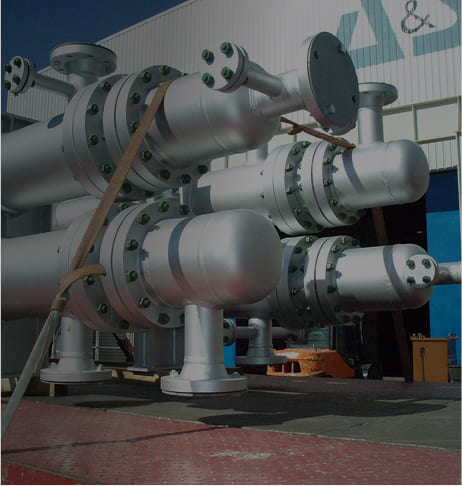
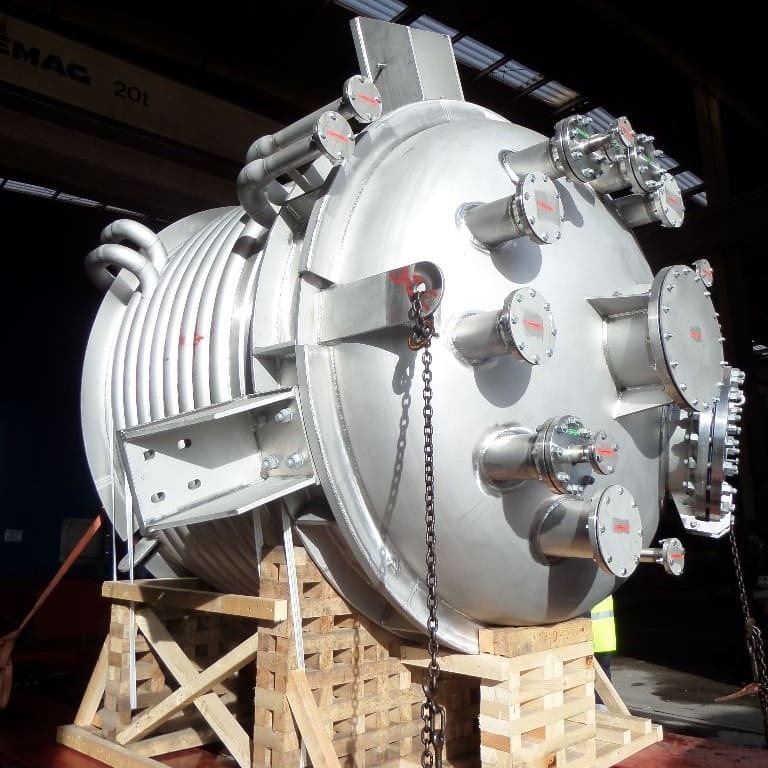
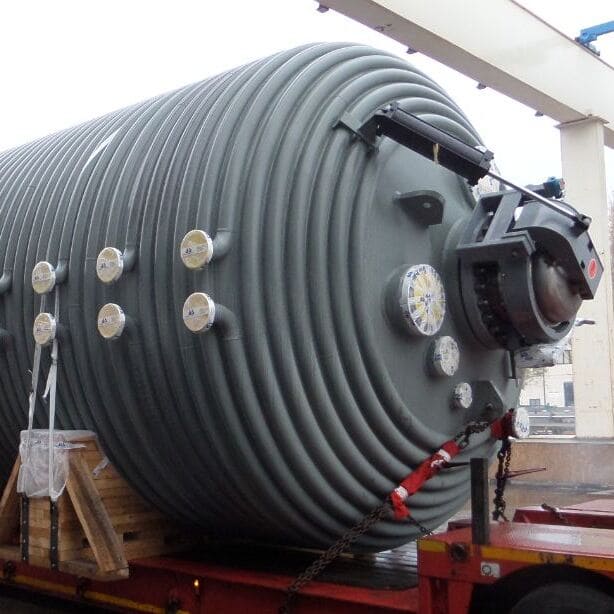
- Reactors can be equipped with cooling or heating systems, including jackets, half coils, internal coils, dimple jackets, and electrical tracing, for precise temperature regulation, making every jacketed reactor suited to tightly controlled exothermic or endothermic reactions.
- Available with or without agitation systems, designed to enhance reaction efficiency and optimize mixing, supporting both agitated reactor and static vessel configurations.
Batch and Continuous Reactor Solutions
InoxTorres manufactures both batch reactors and continuous flow reactors (including CSTR configurations) to match your production method. Batch reactors offer flexibility for lower-volume, high-value chemical and pharmaceutical production runs, while continuous reactors support high-throughput petrochemical and fine chemical processes that demand consistent, around-the-clock output. Every pressure reactor, whether batch or continuous, is custom-engineered to your temperature, pressure, and material specifications.
Industrial Applications
Reactors are essential for facilitating a variety of complex chemical reactions under precisely controlled conditions. Typical applications include distillation, polymerization, oxidation, and crystallization, where precise control of temperature, pressure, and reaction time is vital to achieve optimal results.
- Petrochemical Industry: used for polymerization, pyrolysis, and distillation reactions, essential for producing petrochemical derivatives. Our petrochemical reactors are built to withstand corrosive feedstocks and extreme operating temperatures found in refining and derivative processing.
- Pharmaceuticals: employed in batch reactors for drug synthesis, ensuring precise control over temperature and reaction time. These pharmaceutical reactors support the sterility, traceability, and documentation requirements critical to GMP manufacturing environments.
- Chemical Processing: used in various chemical reactions such as oxidation, crystallization, and polymerization. Our chemical reactor vessels are engineered to handle corrosive media safely across continuous production lines.
- Fine Chemicals: applied in continuous processes for fine chemical production, where high precision and control are required, supporting the tight tolerances fine chemical manufacturers rely on for consistent batch-to-batch quality.
Innovative Reactor solutions for high-efficiency processes
At InoxTorres Group, we prioritize delivering reactors that meet and exceed industry expectations. Our reactors are designed for maximum efficiency, ensuring consistent performance even under the most challenging conditions. By tailoring each reactor to specific chemical processes, our clients benefit from optimized energy use, reduced operational costs, and enhanced productivity. With advanced manufacturing techniques, we provide solutions that ensure long-term durability, minimal downtime, and seamless integration into complex industrial setups. As an experienced reactor manufacturer, we support clients from initial process design through fabrication, testing, and delivery — backed by our quality management system and international certifications.
- Energy Optimization: custom designs that ensure efficient energy use, reducing operational costs and improving overall productivity.
- Enhanced Durability: robust reactors built to withstand the toughest industrial environments, minimizing maintenance and downtime.
- Tailored Solutions: reactors customized to meet specific process requirements, ensuring seamless integration and optimal performance.
Get in touch with us. We're here to assist you.
Looking for a custom reactor manufacturer that can match your exact pressure, material, and process requirements? Whether you need a stainless steel reactor, titanium reactor, or ATEX-rated jacketed reactor for petrochemical, pharmaceutical, or fine chemical production, our engineering team is ready to design a solution built around your specifications. Contact our team to discuss your project.
FAQ
What types of chemical reactions can your reactors handle?
InoxTorres reactors are engineered to handle a wide variety of chemical reactions, including polymerization, oxidation, distillation, crystallization, and extraction. Available as batch reactors or continuous-flow reactors, each unit is custom-built in stainless steel, duplex, or titanium to match the specific chemical, thermal, and pressure requirements of your process.
What is the maximum pressure your reactors can handle?
InoxTorres manufactures both low-pressure and high-pressure reactors, with maximum ratings determined by the reactor’s design, wall thickness, and materials. Our pressure reactors are custom-engineered to meet international design codes such as ASME and EN-13445, ensuring safe, compliant performance in demanding chemical and pharmaceutical processes.
What materials are your reactors made from?
InoxTorres designs and manufactures reactors from stainless steel, high-nickel alloys, duplex, superduplex, titanium, and clad materials. Material selection depends on the specific chemical process, operating temperature, pressure, and required corrosion resistance, allowing each stainless steel reactor or titanium reactor to be precisely tailored to your application.
What size reactors do you manufacture?
InoxTorres manufactures reactors in a wide range of sizes, from small-scale units to large industrial reactors weighing up to 300 tons. Each custom reactor can be engineered with diameters up to 8 meters and lengths up to 50 meters, ensuring the right fit for petrochemical, pharmaceutical, and chemical processing applications.
Are InoxTorres reactors certified for use in hazardous (ATEX) environments?
Yes. InoxTorres reactors are available with ATEX-compliant insulation and configurations designed for safe operation in explosive atmospheres. Combined with agitation systems, heating and cooling jackets, and certified welding, our industrial reactors meet strict international design codes, making them suitable for high-risk chemical, fine chemical, and pharmaceutical manufacturing environments.